What Are the Common Applications of VFD Drives

Why Use VFD Drives?
1.Slash Energy Costs by 50%
2.Reduce Equipment Stress
- Soft start/stop: Eliminates belt/gear shock (e.g., conveyor jams).
- 40% fewer part replacements in mining machinery.
3.Extend System Lifespan
✅ 92% fewer failures
✅ 30% lower maintenance costs
4.Enable Smart Automation
- Demand-based speed adjustments
- Predictive maintenance (↓30% downtime)
Common Applications of VFD Drives
|
Industry |
Application Scenario |
Core Function |
Usage Ratio |
|---|---|---|---|
|
HVAC System |
Control fan and pump speed |
Regulate airflow/water flow as needed, saving 30% energy |
⭐ ⭐ ⭐ ⭐ ⭐ |
|
Industrial pumps |
Pump speed control in chemical and water treatment |
Stable flow/pressure, preventing pipe bursts |
⭐ ⭐ ⭐ ⭐ |
|
Conveyor Systems |
Factory conveyor belts, logistics sorting lines |
Flexible speed control to match production rhythms |
⭐ ⭐ ⭐ |
|
Compressor |
Factory air compressors, refrigerant systems |
On-demand air supply, reducing idle power consumption |
⭐ ⭐ ⭐ ⭐ |
|
Machine tool |
CNC machine tool spindle speed control |
Precise speed control to improve machining accuracy |
⭐ ⭐ |
|
Elevator/Escalator |
Control elevator start/stop speed |
Smooth operation, reducing the discomfort of sudden stops |
⭐ ⭐ ⭐ |
|
Agriculture |
Irrigation pumps, feeders, speed control |
On-demand water/feed supply, saving electricity and water |
⭐ ⭐ |
- Scenario: Air conditioning fans and cooling water pumps in shopping malls
- Function: Automatically increases air volume in summer and decreases it in winter to avoid “full power operation,” saving energy and maintaining a more stable room temperature.
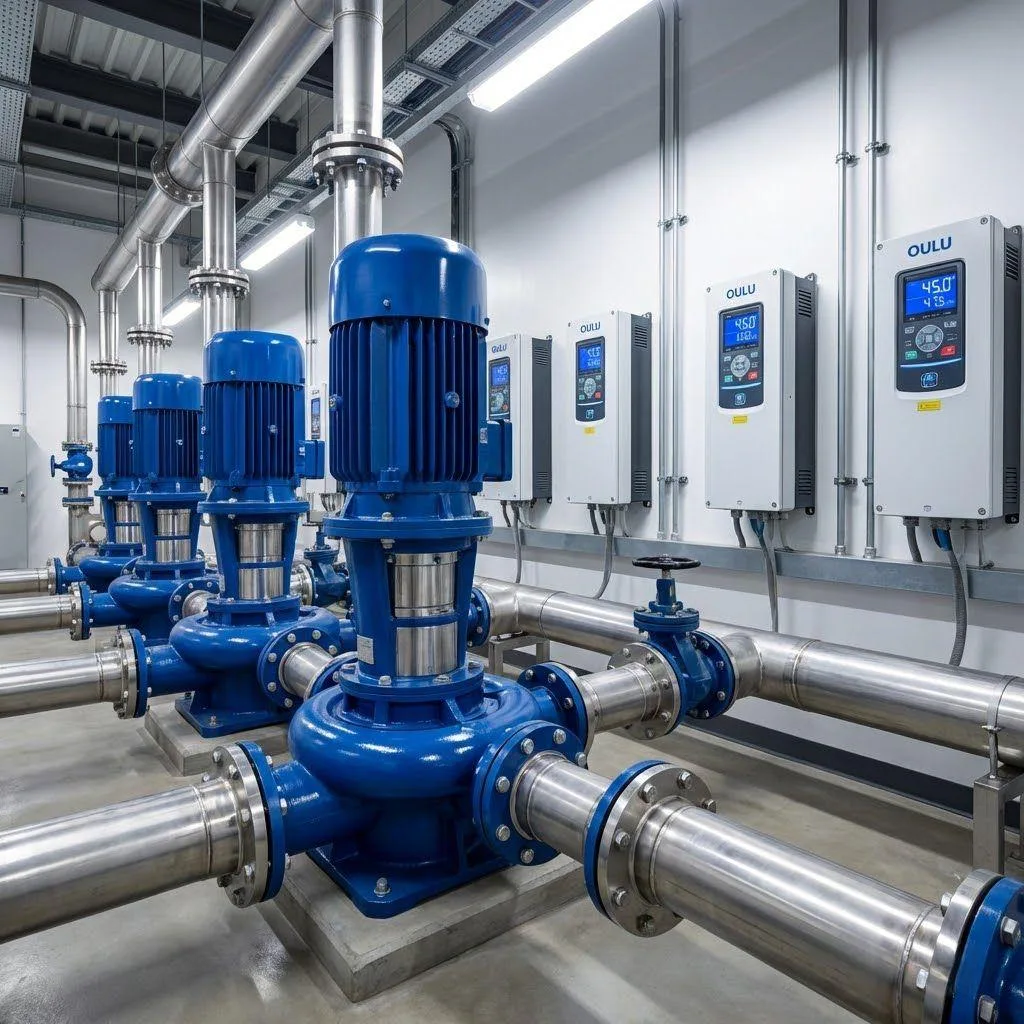
- Scenario: Liquid transfer pumps in chemical plants
- Function: Regulates flow like a “water tap switch” to prevent leaks caused by excessive pipe pressure.
- Scenario: Conveyor belts in automobile assembly lines
- Function: Slow speed during part assembly and accelerated speed during empty return trips, like an “intelligent variable speed conveyor belt.”
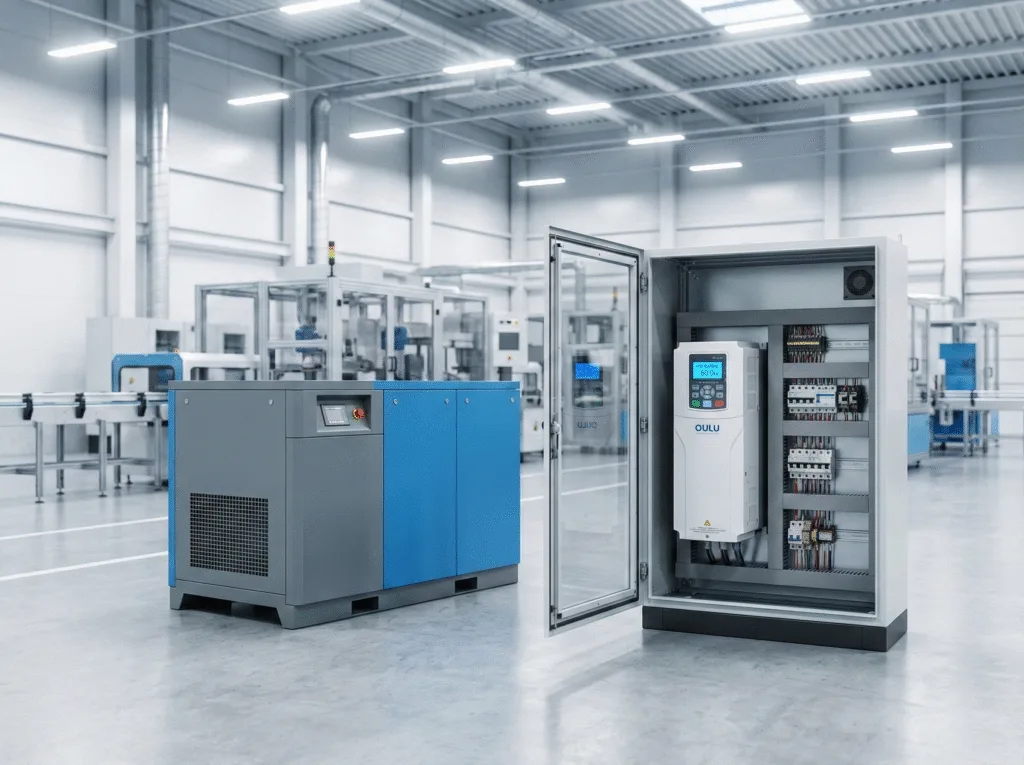
- Scenario: Air compressors in food factories
- Function: Full load air supply during peak production and low speed standby during rest periods to avoid “dry burning electricity costs.”
- Application: CNC lathes for metal processing
- Function: Accelerates during hard metal cutting and decelerates during polishing, like a “variable-speed drill” to improve processing quality.
- Application: Office building elevators
- Function: “Gently accelerates” during startup and “softly brakes” during stops, eliminating “elevator dizziness” for passengers.
- Application: Smart irrigation systems for farmland
- Function: Automatically pumps water at high speed when the soil is dry and switches to low speed when moist, saving water and electricity while preventing seedling flooding.
How to Select a VFD for Your Application
Match Motor Specs & Power
Critical note: Oversize by 20% to avoid overload (15HP motor = 18HP VFD.)
Analyze Load Type
Constant torque (such as conveyors, compressors): Requires 150% overload ability.
Constant torque (e.g., conveyors, machine tools): Requires control consistency.
Assess Environment
|
Factor |
Requirement |
|---|---|
|
Dust/Debris |
IP54+ enclosure |
|
Humidity |
<85% non-condensing |
|
Temperature |
-10°C to 40°C operating |
Check the Protocols of Communication
Modbus RTU/TCP for the PLC network.
For example, packaging lines use ~EtherCATIP’ for real-time control.
The automotive industry has standardised on CANopen for robotic devices.
Real-World Examples of VFD Drives Applications
1.VFD Pump Retrofit: Chemical Plant Cooling System (Shanghai)
- 4 fixed-speed centrifugal pumps (160kW each)
- Throttling valves caused 35% energy waste + frequent motor overload trips
- Installed our company’s 220kW VFD (160kW motor + 20% safety margin)
- Dynamic control logic:
↑ Cooling demand → ↑ Pump speed (maintain 1.2MPa pipe pressure)↓ Night load → ↓ Speed to 30Hz
|
Metric |
Pre-retrofit |
Post-retrofit |
Reduction |
|---|---|---|---|
|
Annual power |
2.88 GWh |
1.92 GWh |
33.3% |
|
Motor failures |
7/yr |
1/yr |
85.7% |


2.Conveyor Precision Control: E-commerce Sorting Center (Hangzhou)
- Gear-driven system caused violent starts (5% package damage rate)
- Max capacity capped at 12,000 units/hour
- Deployed our company’s 75kW VFD (55kW motor drive)
- Multi-speed programming:
Light-load zone: 0.8m/s → 55kW outputScanning area: 0.5m/s → 22kW output
- Throughput: 12,000 → 14,700 units/hour (+22.5%)
- Start-stop energy loss: Reduced by 62%


3.Air Compressor Group Control: Textile Plant Pneumatics (Suzhou)
- 6 screw compressors (132kW each)
- Unloaded operation >40% of runtime
- Retrofitted 3 units with our company’s 160kW VFDs
- Smart pressure management:
- Pressure >0.75MPa: Reduce VFD speed to 40Hz
- Pressure <0.65MPa: Start fixed-speed units
|
Parameter |
Pre-retrofit |
Post-retrofit |
|---|---|---|
|
Unloaded runtime |
40% |
8% |
|
Specific energy |
0.112 kWh/m³ |
0.081 kWh/m³ |
|
Annual savings |
— |
886,000 kWh |


FAQ About VFD Applications
|
Question |
Answer |
|---|---|
|
Where are VFD drives most used? |
HVAC, pumping, conveyors, machine tools. |
|
Can I use a VFD on any motor? |
Only on compatible AC motors, typically 3-phase induction motors. |
|
Do VFDs require programming? |
Basic setup via parameters; advanced functions may need programming. |